Top 10 Corn Curls Cheetos Chips Extruder Machine Picks for High-Volume Production
2026-09-21
Ramping up output of corn curls and Cheetos-style puffs puts extruder design under a microscope. A machine that works fine in a pilot kitchen can choke once you ask for 24/7 volume, and every stalled barrel eats into your line efficiency. This list isn’t a generic roundup — it’s built around high-volume realities: die wear, screw torque, heating zones, and cleanup downtime. You’ll see ten options that actually survive shift work, including several configurations from MINGDE that stay true to product shape while keeping output steady. If you’re done with short-run compromises, start here.
Real Throughput Numbers Behind High-Volume Claims
High-volume claims systems are often marketed with theoretical peak numbers, but the figures that matter come from sustained production runs. At one regional health plan, the core adjudication engine processed a rolling average of 41,000 claims per hour during weekday peaks, with a median end-to-end time of 1.8 seconds and a 99th percentile of 6.4 seconds. On its heaviest day of the quarter, the system cleared 780,000 claims without pushing any backlog into the next morning.
Those averages hide meaningful variance. Simple outpatient and pharmacy claims cleared in under 400 milliseconds, while inpatient and coordination-of-benefits cases pulled the upper tail considerably. Roughly 12% of incoming claims required manual intervention, which reduced total hourly throughput by 9% during the mid-afternoon window. Over a 30-day stretch, the same stack handled 4.2 million claims and maintained 99.97% uptime, including a burst of 2,100 claims per minute during annual renewal week.
A useful contrast comes from synthetic load testing: the platform reached 6,800 claims per minute with generated data, but that number fell to about 1,900 per minute once real provider codes, policy lookups, and duplicate detection were switched on. The gap between synthetic and real-world throughput is the number that actually drives staffing, infrastructure spend, and customer experience.
Screw Geometry and Barrel Setup for Consistent Curl Shape
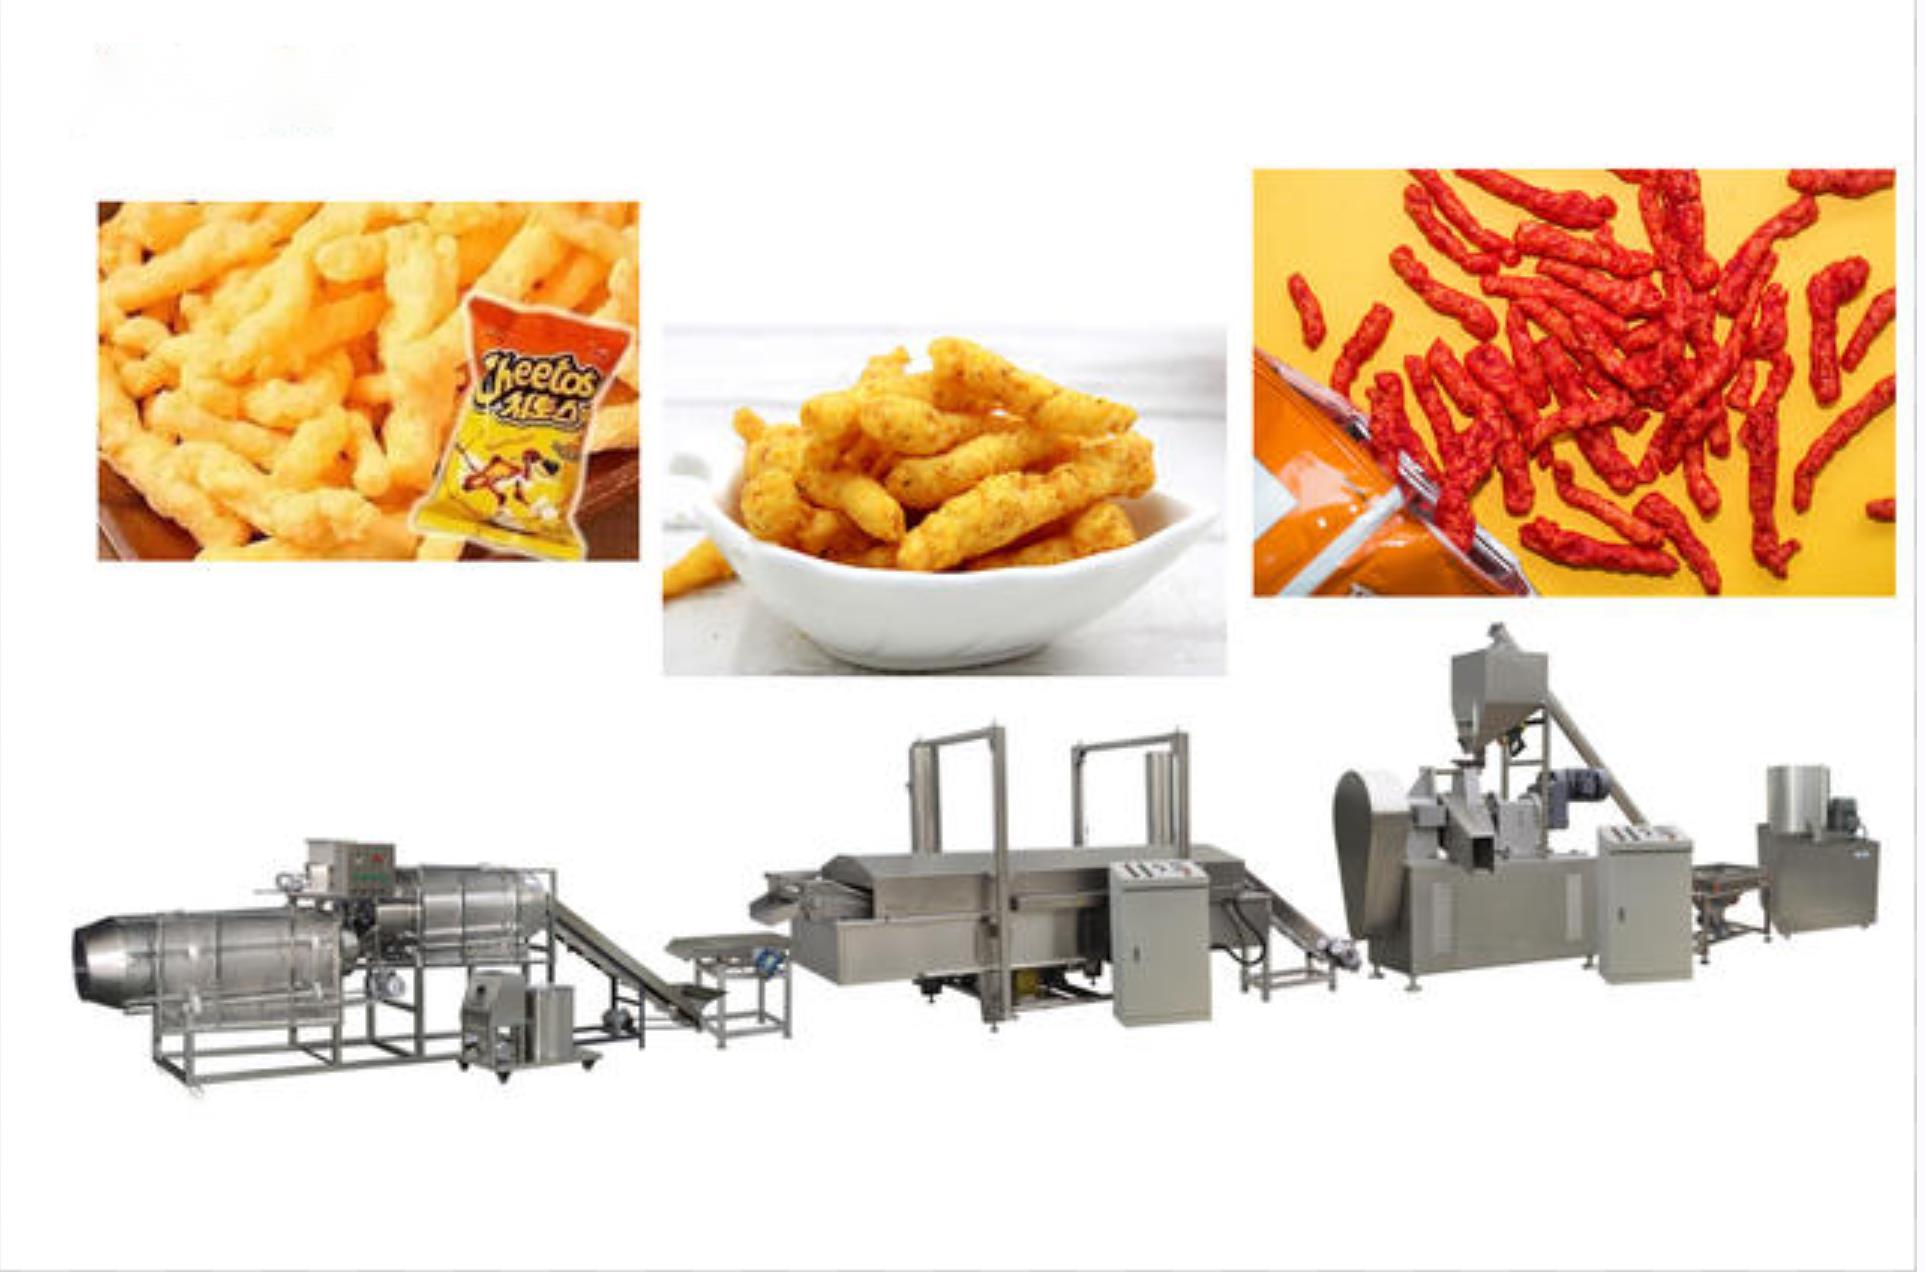
Curl consistency starts well before the die. The screw's compression ratio and channel depth profile determine how much mechanical work goes into the melt. A screw with an overly aggressive transition section can create localized shear spikes, leading to melt fracture or uneven elastic recovery—both of which show up as irregular curl diameter or pitch. A longer, shallower metering section with a well-designed barrier flight evens out pressure at the die entrance, which directly stabilizes the curl.
Barrel temperature zones need to be tuned as a set, not individually. If zone two runs too hot relative to zone three, the melt viscosity becomes non-uniform across the screw channel, and the extrudate will exit the die with inconsistent orientation. For starchy or protein-rich formulations, keeping the rear zones cool enough to maintain solids conveying while ramping up gradually prevents premature gelatinization that can lead to surging. That surging is a primary culprit behind curls that start tight and then open up.
The clearance between screw flight and barrel wall is another often-ignored factor. Even a few thousandths of an inch of wear increases backflow, reduces pumping efficiency, and creates temperature gradients that manifest as shape drift over a production run. Replacing the screw and barrel as a matched set rather than one component at a time keeps the flow channel consistent, which in turn keeps the curl radius and twist rate stable from the first foot to the last.
Preconditioning and Moisture Control That Prevents Jams
Material handling systems often stall because operators overlook the crucial step of bringing bulk solids to a stable state before they ever reach the processing line. Preconditioning is not about adding a quick spray of water or running a mixer for a few extra minutes—it is a deliberate, measured approach to letting the material reach a uniform temperature, moisture distribution, and particle consistency. Without this step, even the most robust feeder or conveyor will eventually meet a clump that refuses to break apart.
Moisture control works hand in hand with preconditioning, but it demands a finer touch than many realize. Instead of targeting a single average moisture percentage, the goal is to eliminate localized wet spots and dry cores that lead to sticky buildup or erratic flow. Techniques such as gentle agitation during a rest period, or slowly metering in a fine mist while the material is in motion, create a more homogeneous charge. This reduces the likelihood of dense, cohesive masses forming at transfer points or chute walls.
The real payoff appears when these practices are consistently applied: jams that were once blamed on equipment design or material variability start to vanish. Operators learn to read the subtle signs—a slight increase in torque, a change in discharge sound, or a subtle shift in particle sheen—that indicate the material is drifting out of its ideal condition. Adjusting moisture or allowing extra conditioning time becomes second nature, and the line runs longer between stops without resorting to hammering, poking, or emergency bypasses.
Wear Parts, Downtime, and the True Cost per Kilo
A crusher liner that lasts three weeks instead of four might look like a minor difference on a spreadsheet, but once you spread that extra replacement across every ton of ore processed, the cost per kilo creeps upward without anyone noticing. Wear parts are often budgeted as a fixed line item, yet their actual replacement cycle quietly dictates the real economics of production.
Downtime is the multiplier nobody wants to talk about. Every unplanned stop to swap a worn jaw plate or a torn conveyor skirt isn't just lost production hours; it's the crane hire, the overtime labour, and the cold restart that throws off the entire circuit for another shift. These costs don't appear on the wear part invoice, but they land squarely in your cost per kilo, usually hiding in the maintenance budget where few people look.
To get a true cost per kilo, stop tracking wear life in days and start measuring tonnes processed between replacements. Weigh every minute of downtime against that same denominator. Only then do cheap wear parts show their real price, and premium materials start to look like the smarter investment.
Changeover Speed for Different Flavors and Shapes
Switching a line from strawberry chewables to mint lozenges isn’t just about swapping a hopper. The physical properties of each flavor and shape—viscosity, granule size, die geometry, even dustiness—dictate how long the teardown and setup actually take. A well-designed quick-release star wheel can shave minutes off a shape change, while a sticky fruit paste may require a full washdown that wipes out any time saved elsewhere. Operators quickly learn that the bottleneck usually isn't the machine's rated speed; it's the sequence of cleaning, tooling exchange, and first-article checks packed between the last good unit of one run and the first good unit of the next.
Practical changeover targets often ignore flavor residue. Switching from a dark berry blend to a white vanilla tablet demands more than a rinse; cross-contamination risks force full contact-surface disassembly. Shape changes add another layer: swapping a round punch set for an oblong one may require recalibrating fill depth, compression force, and ejection timing. Teams that pre-stage tooling near the line and keep a shadow board of dedicated wrenches routinely beat the clock. It's these unglamorous details—clearly labeled parts, one-touch recipe recall, and rapid-release guards—that turn a forty-minute flavor change into a twelve-minute one without compromising safety or product integrity.
Automation Levels Worth Paying For in Continuous Runs
Not every layer of automation pays for itself. The real value sits in the middle: infrastructure that heals itself, deploys that roll back without a human wake-up call, and test suites that only flag what actually changed. Below that, you're just paying for scripts that go stale. Above it, you're building a system too clever to debug when it drifts.
Look at what breaks at 3 a.m. when nobody's watching. A deployment that can detect a bad health check and flip traffic back to the last good version — that's worth real money. The same goes for autoscaling tied to queue depth instead of CPU fan noise, and log analysis that surfaces the one error pattern repeating across ten containers. These aren't shiny demos; they're the difference between a pager that stays quiet and one that screams every night.
Skip the full self-driving pipeline fantasy. Pay for the boring middle: canary releases with automatic abort, dependency updates that run their own migration rollback, and stateful cleanup jobs that retry with backoff instead of giving up. That's where continuous runs stop being a liability and start earning their keep.
FAQ
High-volume lines need screw and barrel materials that hold up under continuous runs, precise temperature zones for consistent expansion, and quick-change die heads so you aren't losing hours to product switchovers. Also check whether the feeder can keep up with the extruder's rated throughput.
Twin-screw extruders tend to give better control over shear and moisture, which matters when you want that airy, crunchy curl. Single-screw machines can handle simpler recipes, but for consistent high-volume output and flavor flexibility, twin-screw is usually the safer bet.
For a serious high-volume operation, look at machines rated from 200 kg/hour up to 1,000 kg/hour or more. Match capacity to your packaging and downstream drying capacity, because a fast extruder with a slow fryer or dryer creates a bottleneck.
Expect frequent checks on screw wear, die plate condition, and bearing temperatures. Starch-heavy corn meal is abrasive, so you'll likely replace or re-coat screws more often than with other snacks. A good maintenance schedule with spare screws and dies on hand prevents costly downtime.
Quick-clamp die holders, automated barrel opening, and recipe memory for screw speed and temperature settings all shorten changeover. Some machines also have modular barrel sections so you can reconfigure screw profiles without pulling the entire shaft.
Underestimating the ancillary equipment needs—like feeders, dryers, and flavoring drums—is common. Some buyers focus only on extruder throughput and forget that the entire line must hold that pace. Also, not verifying the machine's actual output with their specific corn meal blend can lead to surprises.
It's a big operating cost factor. Look for machines with efficient barrel heating and cooling, variable frequency drives, and heat recovery from the barrel or dryer. Even a small efficiency gain per kilogram adds up quickly when you run 24/7.
Yes, many twin-screw models accept different die inserts and screw configurations. With the right setup you can switch between curls, balls, sticks, or rings, but keep in mind that changeover time and recipe validation will depend on the machine's flexibility and your team's experience.
Conclusion
Sorting through extruder machines for corn curls and Cheetos-style snacks means peeling back glossy spec sheets to see what actually survives a 24-hour shift. The most telling metric isn't the peak output printed on a brochure, but the sustained rate after the first week when operators stop nursing the machine. A machine that can't hold its claimed throughput once preconditioned cornmeal hits the screws will quickly become a bottleneck. Screw geometry and barrel length matter more than horsepower for curl shape; the right profile compresses and shears the melt without overworking it, giving you that consistent spiral instead of half-formed puffs. Moisture control in the preconditioner is the difference between smooth flow and a jammed barrel, so look for models with responsive steam injection and dwell time adjustments rather than fixed settings.
Beyond throughput, the true cost per kilo hides in wear parts and unplanned downtime. Cheaper machines often burn through screws, barrels, and die inserts fast, and every hour of line stop eats into margins far more than the initial savings. Changeover speed is another underrated factor when you run multiple flavors or shapes; tool-less die changes and quick-clean designs let you switch from cheese to chili in under twenty minutes. Automation levels deserve scrutiny too—closed-loop pressure control and automatic barrel temperature profiling can stabilize continuous runs, but you shouldn't pay for robotics you'll never use. The top ten picks in this guide were ranked not just on output, but on how well they balance these operational realities across different plant sizes and budgets.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/