Ultrasonic Coating System Factory Insights: Exploring Advanced Manufacturing Processes Behind Reliable Coating Equipment
2026-09-25
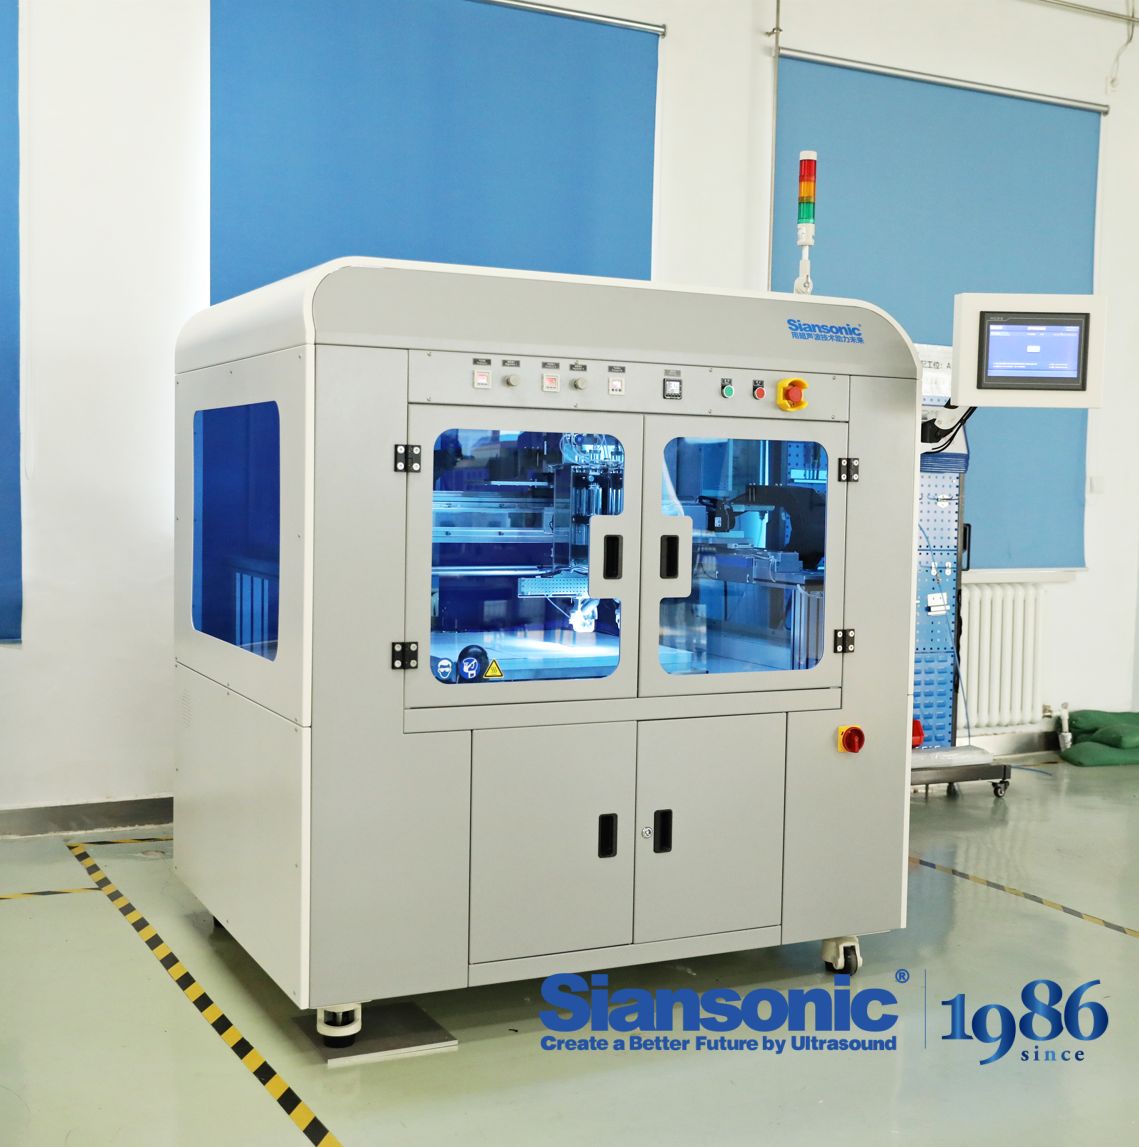
Every reliable ultrasonic coating system starts long before the first spray test. Inside the Siansonic factory, the real story unfolds across precision-machined nozzles, tightly controlled transducer assembly, and a production floor where tolerances are measured in microns—not millimeters. This isn’t just equipment manufacturing; it’s a quiet obsession with repeatability. As we walk through the processes that turn raw piezoelectric ceramics and titanium alloys into coating tools trusted by R&D labs and high-volume lines alike, one question keeps surfacing: what exactly separates a dependable system from a disposable one? The answer lies in the factory details most buyers never see.
Where Nozzle Geometry Gets Its Final Tuning
The last tweaks to a nozzle’s shape rarely happen on a drawing board. They come from measured flow data, captured while the part is clamped to a bench and fed with compressed air or water. Small changes in the throat radius or the divergence angle are filed, polished, or shimmed until the discharge pattern matches what the math promised.
Thermal growth and material springback also leave their fingerprints here. A nozzle machined to nominal dimensions will settle into a slightly different contour once it heats up or relaxes after clamping. Final tuning accounts for that drift by biasing the profile a few microns in the opposite direction, usually guided by repeated measurements on the same fixture.
Operators who do this work tend to rely on tactile feedback and accumulated notes rather than a strict recipe. Each batch of material behaves a little differently, so the final pass may involve hand-lapping the exit edge or adjusting the surface roughness to shift the breakup length of a jet. That hands-on step is where a good design becomes a repeatable part.
Surface Prep Routines That Make or Break Adhesion
Abrasion alone won't save a weak bond. The real separator between joints that hold and those that fail under light load is the sequence of wipe, abrade, wipe again, and verify. Many shops skip the final check, assuming a clean-looking surface is ready. It rarely is. Solvent residue, invisible oxidation, or a thumbprint can create a slick micro-layer that adhesive simply floats on. The routine that makes adhesion predictable is boring but non-negotiable: remove gross contamination, mechanically break the gloss, remove the dust and oils that abrasion exposes, then test with a water break or dyne pen before any adhesive leaves the tube.
Temperature matters more than most people admit. Prepping a cold substrate and then applying a room-temperature adhesive is a setup for a weak interphase. The surface must be above dew point, and ideally in the same range as the adhesive's cure profile. A quick heat gun pass before final wipe can drive off condensed moisture, but don't overdo it — overheating can oxidize metals or soften plastics and change surface energy in the wrong direction. The goal is a surface that is dry, slightly warm to the touch, and chemically active, not one that's been cooked into a new material.
Don't trust a generic prep for every substrate. Polypropylene and polyethylene need flame, plasma, or corona treatment because mechanical abrasion just smears the low-energy surface. Aluminum benefits from a light phosphoric acid etch or conversion coating, not just sanding. Glass wants a silane primer after cleaning. The routine that breaks adhesion is the one-size-fits-all approach. The one that makes it is a short, documented sequence that respects the chemistry of the exact materials in your hand.
The Calibration Room Stories Behind Repeatable Microns
Tucked behind a double set of steel doors, the calibration room hums at a frequency most people never notice. Here, a micron is not just a number on a screen—it is a negotiation between temperature, vibration, and the stubbornness of metal. Every gauge block, every dial indicator, arrives with a story of wear and drift, and the job is to listen before chasing zero.
Repeatability does not live in the machine alone. It grows from the rituals that rarely get written down: waiting for the room to settle after a delivery truck rumbles past, wiping a ceramic anvil with a cloth that has been washed a hundred times, checking the same dimension three times not because the first two were wrong, but because the third one teaches you what the first two actually meant. Small choices, repeated until they vanish into instinct, are what keep a measurement honest from Monday to Monday.
The real story inside those climate-controlled walls is not about perfect instruments. It is about people who refuse to let a few microns become an excuse. When a process drifts by four thousandths of a millimeter, nobody panics; they trace the thread back through air pressure, hand temperature, and the subtle flex of a fixture. That patience turns a cold room into a place where repeatability becomes less a specification and more a habit.
Power Supply Behavior Beyond the Spec Sheet
A spec sheet will tell you a unit can deliver 750 watts, but it won't mention how it reacts when a GPU suddenly pulls an extra 200 watts in a millisecond. In practice, the voltage may dip enough to cause a reboot, even if the average load never comes close to the label. This transient response is a better indicator of real-world stability than the continuous wattage number, and it's rarely published.
Another field-only behavior is the hold-up time under a brownout. On paper, the bulk capacitor might be rated for 16 ms, but as components age, that cushion shrinks. In areas with frequent line flicker, a two-year-old supply can drop out long before a UPS kicks in, while a fresh unit from a different brand shrugs off the same event. Thermal derating curves also matter more than the 40°C rating implies, because most cases don't deliver test-bench airflow.
Beyond that, fan profiles and coil whine rarely appear in datasheets. A supply that stays silent at 50% load may emit an irritating buzz when paired with a particular motherboard's VRM switching frequency. Cross-load behavior—how the 12V rail behaves when the 5V rail is nearly idle—can also shift by several percentage points depending on the internal topology, something you only discover after installation.
Cleanroom Habits That Protect Coating Integrity
A surprising number of coating failures trace back to small, everyday movements inside the cleanroom. Rubbing your nose, adjusting a face mask, or even folding your arms can release particles that settle on a freshly coated surface. The habit of keeping your hands below chest level after gowning, and never touching your face or street clothes, does more for coating integrity than any amount of post-process inspection. If you feel an itch or need to reposition a tool, step away from the coating area first.
How you handle substrates and fixtures matters just as much as what you wear. Gloves should be changed whenever they come into contact with door handles, chair backs, or the outside of a storage cabinet. Oils from fingerprints, even through a glove, can create invisible bond breakers under a coating. Wiping down all contact surfaces with the approved solvent before placing a part down, and never resting coated items on unverified surfaces, is a habit that prevents peeling and fisheyes later.
Airflow is not something to fight or ignore. Rushing through doorways, propping open pass-throughs, or standing directly over a wet coating can disrupt the laminar flow and pull contaminants into the work zone. Slow, deliberate movement gives the filtered air time to sweep particles away. At the end of a shift, taking five minutes to close all chemical containers, wipe down benches, and replace tacky mats keeps the room stable overnight, so the next day's coatings start from a clean baseline.
Following One System From First Bolt to Final Sign-Off
There is a quiet discipline in watching a single structure move from raw steel to the last stamped page of a commissioning binder. It means every bolt, bracket, and weld carries the same thread of accountability — not because someone remembered to check, but because the system never allowed it to be forgotten.
On the floor, that looks like torque values logged against serial numbers, paint touch-ups tied to date-coded photos, and cable pulls verified against line diagrams before the next crew arrives. Nothing waits for a heroic memory. The system flags a missed torque the same way it flags a missing signature, so the handoff from electricians to inspectors is just a continuation of the same record, not a fresh start.
By the time final sign-off happens, the paperwork and the physical build have been walking side by side. That is what changes the last day on site: you are not scrambling to prove the work is done. You are simply closing the loop that began with the first bolt.
FAQ
The consistency largely comes from how the factory manages tolerances during nozzle assembly and power delivery calibration. Each system is put through a spray pattern test with a reference fluid, and only units that match the target droplet size distribution within a narrow band move on. This hands-on verification, combined with documented torque settings on ultrasonic transducers, keeps variations low across batches.
Reliability starts with component-level burn-in and stress testing before final assembly. The transducer housings are sealed in a cleanroom environment to prevent contamination at the piezo element interface, and all wetted parts undergo a passivation step to resist chemical attack. Then every machine runs a 48-hour continuous spray cycle with intermittent shutdowns to catch early failures before shipping.
Alignment is critical because the standing wave pattern between the nozzle tip and substrate determines how evenly the droplets distribute. Factory technicians use laser displacement sensors to set the gap within ±0.05 mm for each application head, then lock the gantry positions with matched shims. Even a slight tilt can create banding or edge buildup, so the assembly jigs are re-verified against a master reference every shift.
The coating heads are typically machined from titanium or 316L stainless steel, then subjected to an electropolishing process that removes micro-burrs and improves chemical resistance. For aggressive solvents, wetted surfaces receive a fluoropolymer coating, and O-ring grooves are redesigned with double-seal geometry. This combination prevents corrosion pitting and extends the service interval of the nozzle.
The factory uses a modular platform where the ultrasonic generator, fluid delivery skid, and motion gantry are configured separately. Small lab units share the same core nozzle and transducer as high-volume systems but use a lighter frame and single-axis stage. By keeping the spray head identical across scales, the process parameters transfer directly, and the factory can pre-wire for additional robots or conveyor integration when a customer plans to scale up.
Every completed system sprays a customer-specified or reference coating onto glass coupons, and the factory measures the dry film thickness at a grid of points. The acceptance report includes a heat map of thickness variation and droplet size distribution from a laser diffraction sensor. If any point deviates by more than 3% from the target, technicians adjust the nozzle orientation or fluid pressure and rerun the full panel.
Integration is treated as a mechanical and electrical handshake rather than an afterthought. The factory provides a standard Profinet or EtherNet/IP interface for recipe control, and the frame is designed with dowel-pin locating features that match common robot pedestals. Before shipping, technicians simulate the customer's line speed and trigger sequence using a mock conveyor, so the coating system arrives with all interlock logic already tested.
Operator training is embedded in the factory's quality loop. New assembly technicians spend two weeks on a dedicated training line where they build a complete coating module under supervision, then their work is compared against a golden unit. Because ultrasonic coating depends on tiny mechanical adjustments, the factory maintains a certification matrix for tasks like nozzle lapping and transducer torqueing, and operators must recertify every six months by assembling a test head that passes a full spray audit.
Conclusion
Walking the floor where ultrasonic coating systems come together, the first thing that stands out is how much attention goes into details most spec sheets never mention. Nozzle geometry isn't just machined to a drawing; it's hand-tuned and tested under real flow conditions until the spray pattern settles into a repeatable shape. Surface prep happens in a dedicated bay where operators follow routines that vary not only by substrate but by the day's humidity and batch history, because a few stray molecules of contamination are enough to wreck adhesion. Then there's the calibration room, a quiet space filled with reference standards and logbooks documenting every adjustment made to hold micron-level film thickness across hundreds of cycles.
Power supply behavior rarely mirrors the printed datasheet. On paper, a unit may meet its voltage and frequency specs, but on the bench it can drift under thermal load or interact with transducer impedance in ways that affect droplet size and coating uniformity. That's why every build goes through a burn-in period with data logging that captures performance beyond the official limits. Cleanroom habits matter just as much: technicians follow strict gowning and tool-cleaning protocols to keep particles from embedding in wet film, which would later show up as pinholes or delamination. Following one system from first bolt to final sign-off reveals that reliability isn't a single feature—it's a chain of small, disciplined decisions made from the moment raw stock enters the shop to the last inspection report signed off.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/